Rear End — 5 Hrs
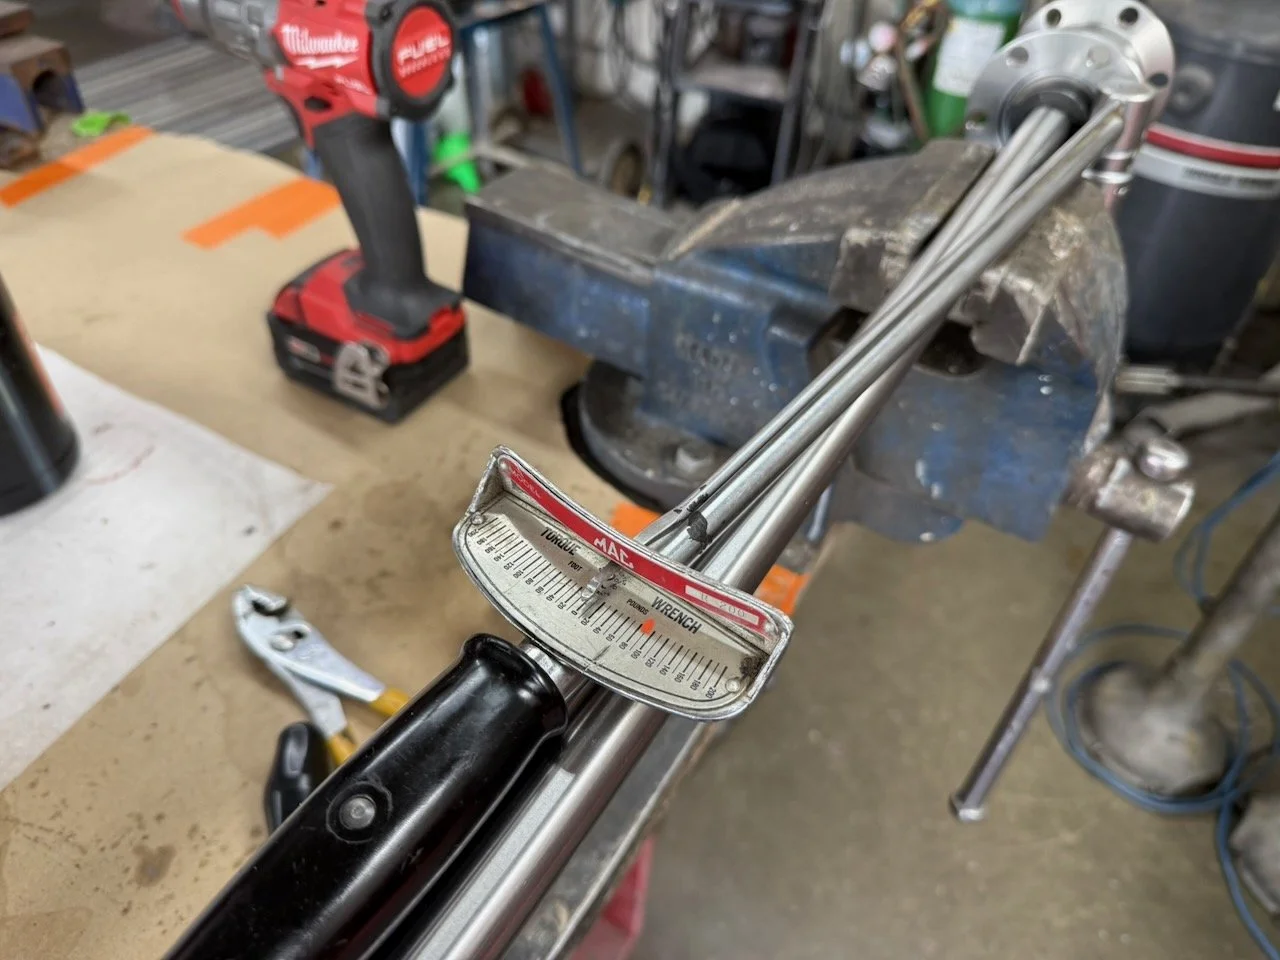
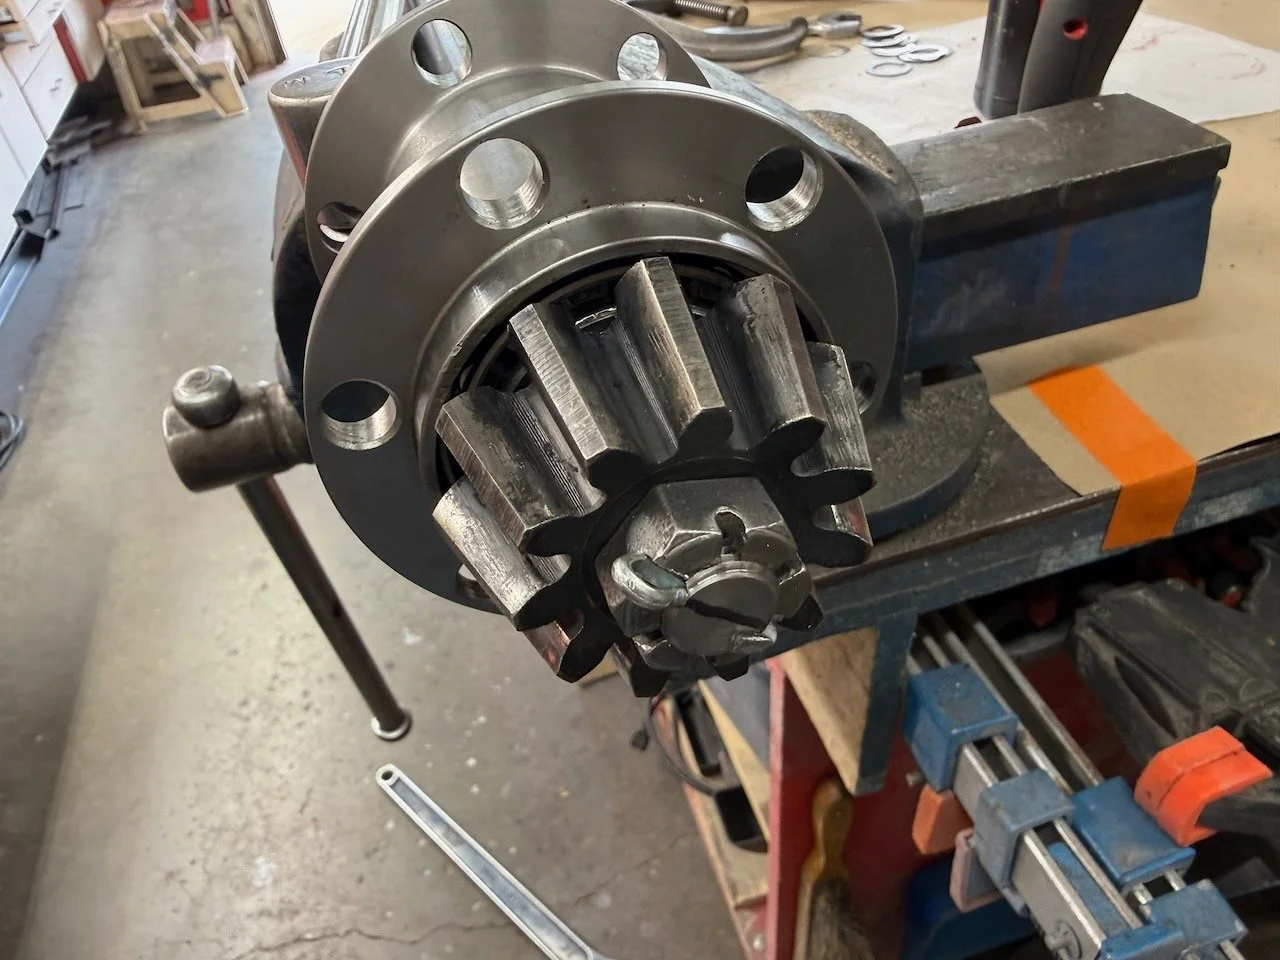
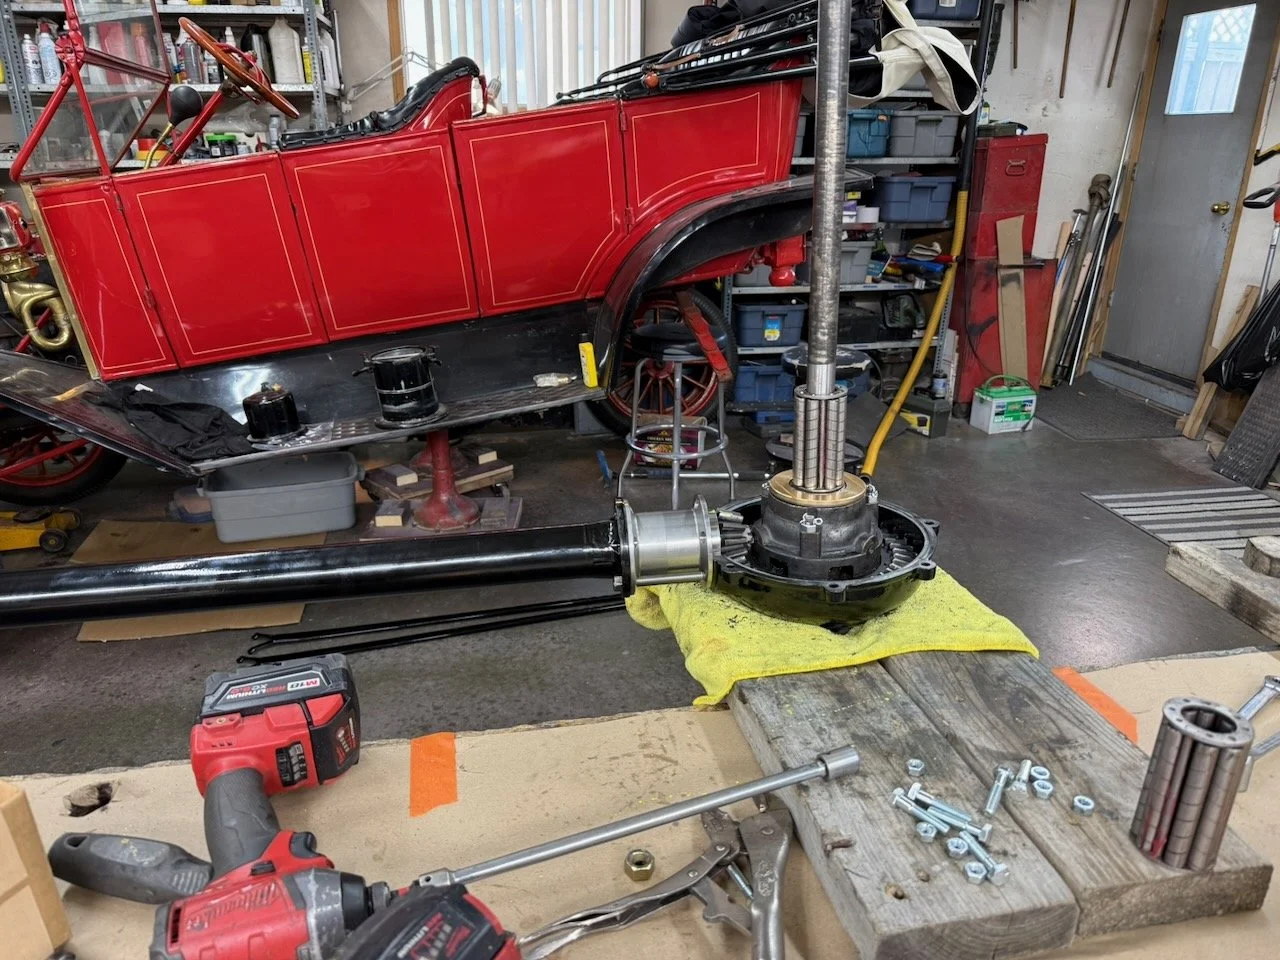
Torqued the pinion gear (75 ft/lbs) and preloaded the bearing.
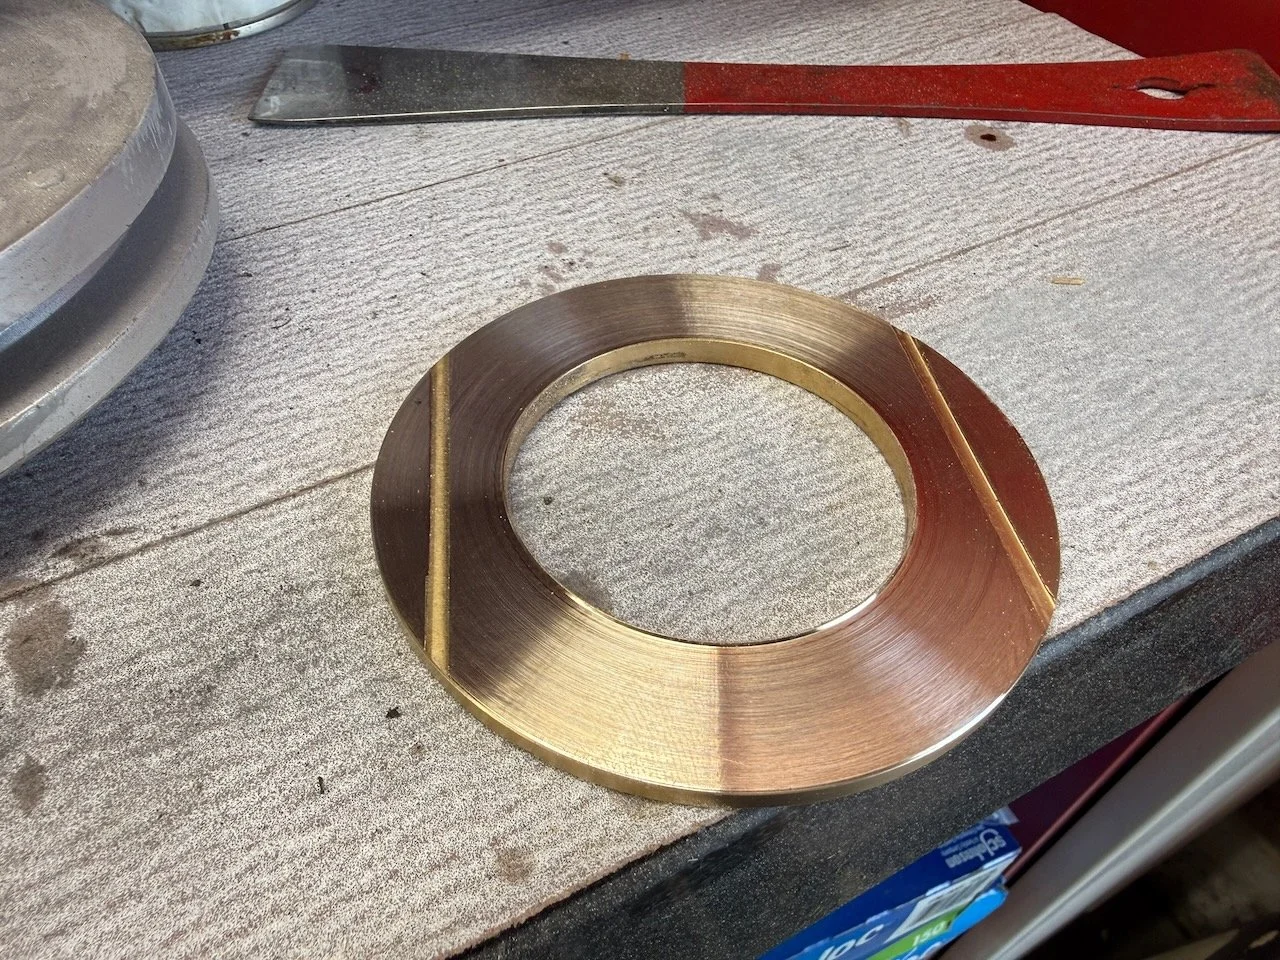
Set the clearance for the right-hand housing by machining the bronze thrust washer. I measured the required clearance using a hardened steel washer and several shims.
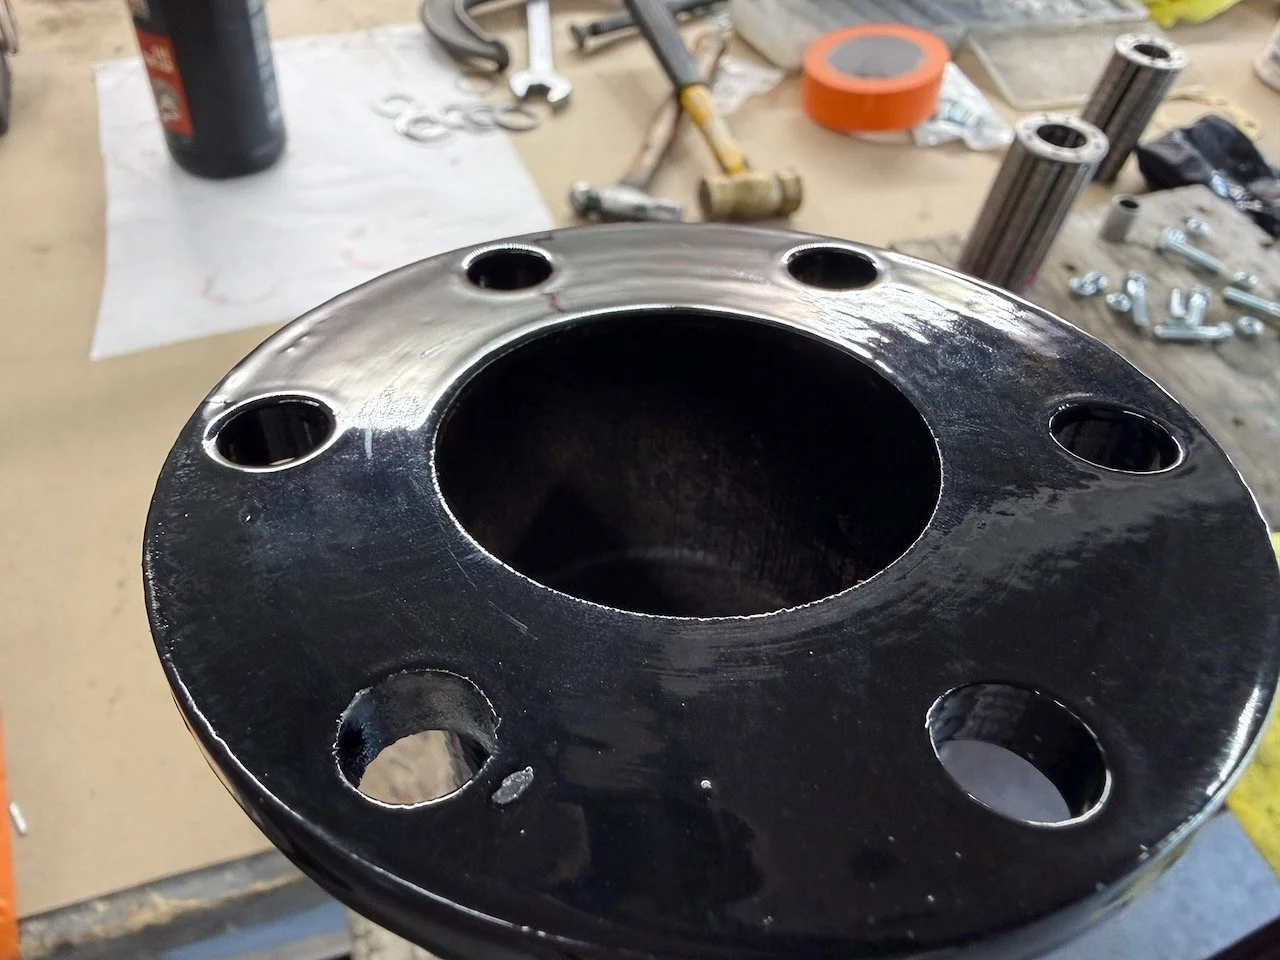
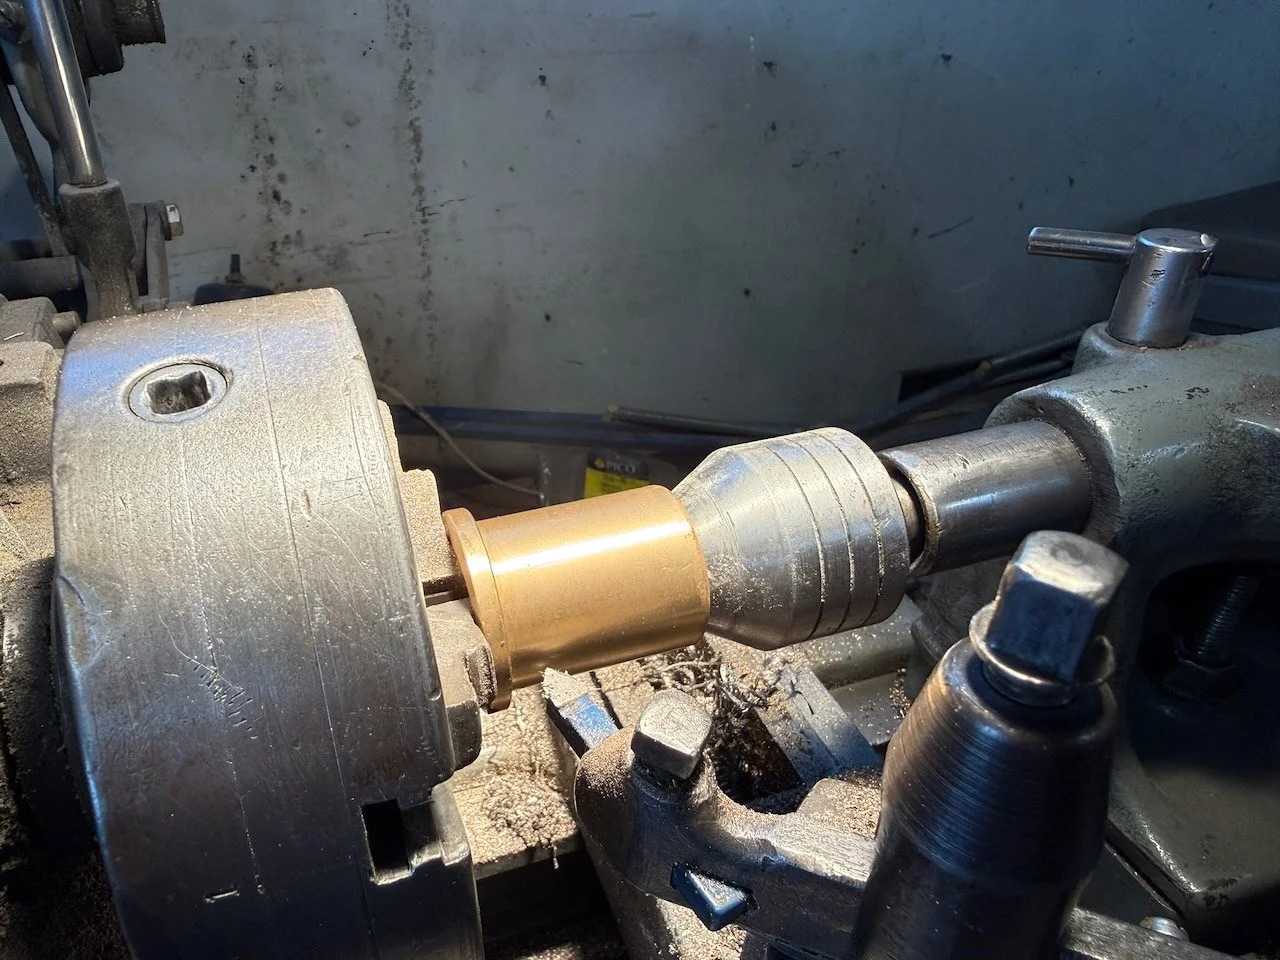
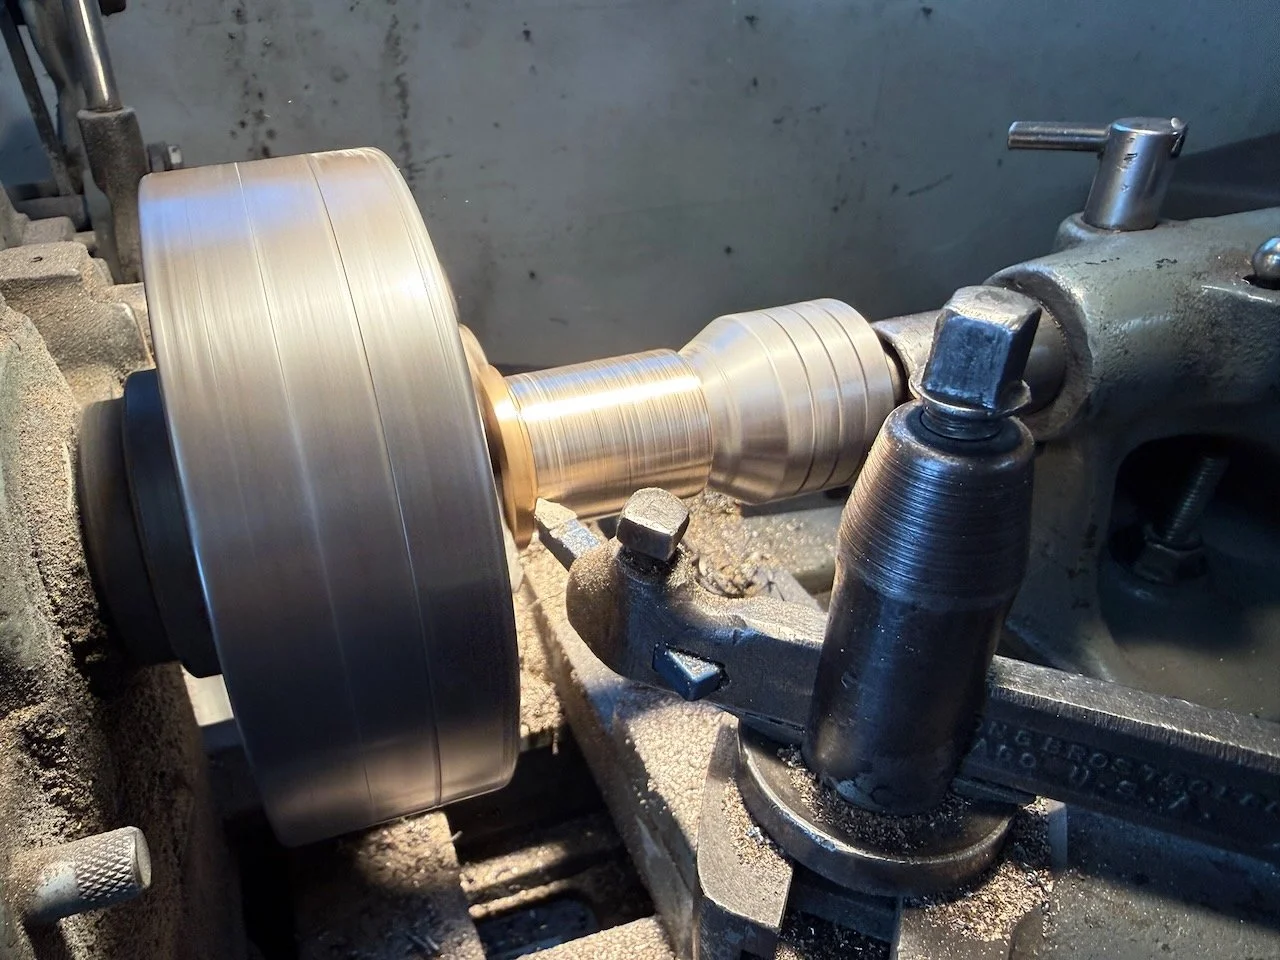
Machined and fit the front driveshaft bushing. I used a belt and suspenders approach, allowing for the proper thrust on the bushing as a backup to the locking collar on the modern pinion bearing at the back.
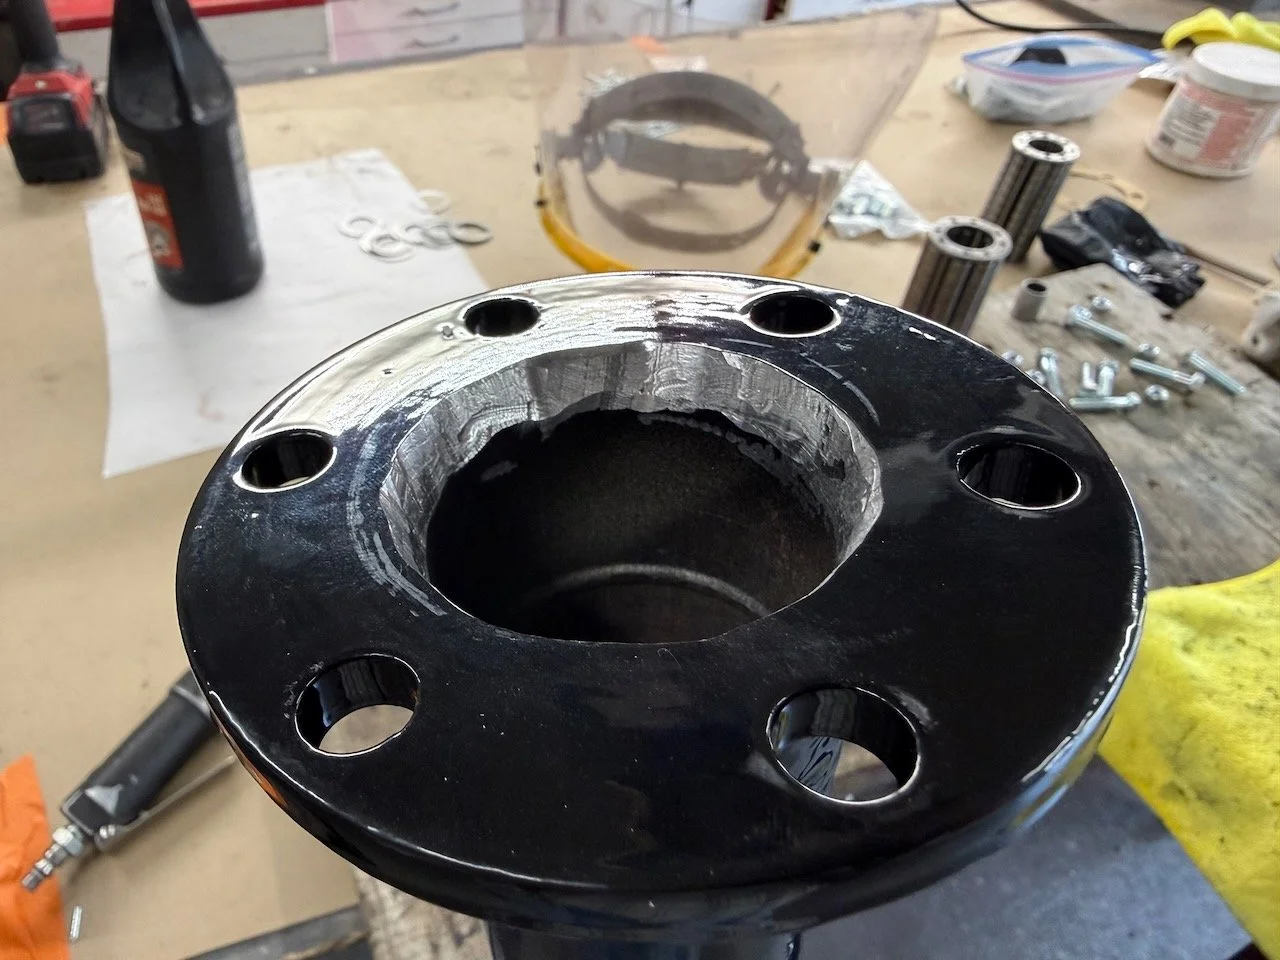
The set screw on the modern pinion bearing locking collar interferes with the inside of the torque tube. I machined the clearance several times and ground the set screw to obtain enough clearance so the driveshaft will rotate without hanging up. Still more work to do on that.